


When Should Pharmaceutical Facilities Consider Dedicated Quarantine Cold Rooms?
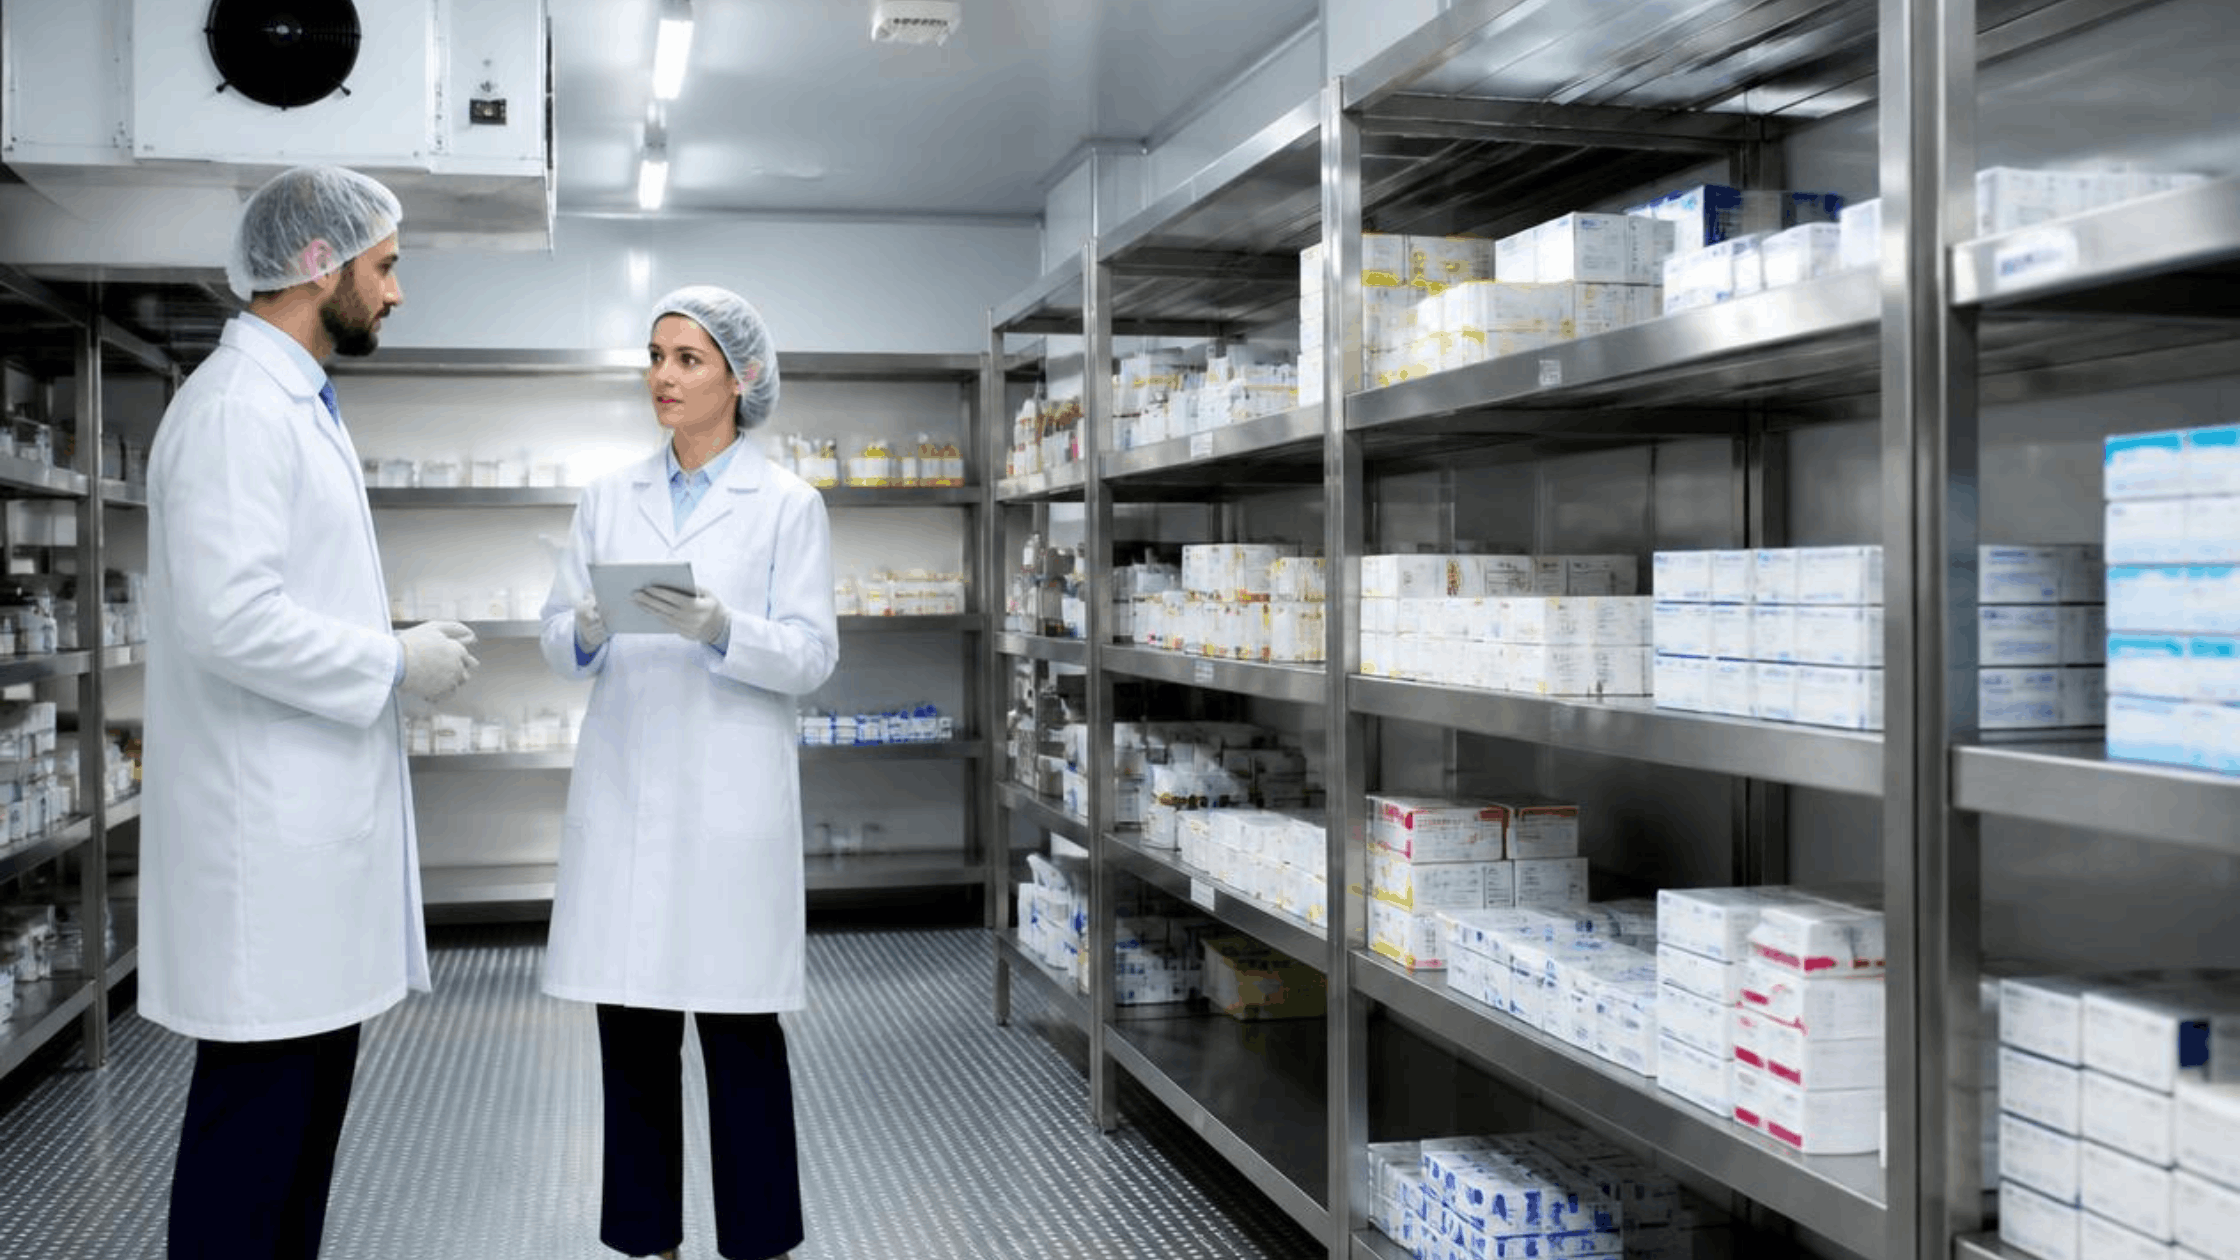
Pharmaceutical products often pass through several stages before they are approved for distribution. Newly received materials, products awaiting quality assessment and returned inventory may all require temporary storage while quality assurance procedures are completed. Managing these products within the same refrigerated environment as released inventory can gradually increase operational complexity, particularly as storage volumes and product varieties continue to grow. Many pharmaceutical facilities initially allocate designated shelving or clearly labelled storage zones within an existing cold room to separate quarantine stock from approved products. While this approach may be sufficient during the early stages of operation, expanding facilities often discover that increasing inventory volumes and more complex workflows require a different storage strategy.
A dedicated pharmaceutical quarantine cold room provides an additional layer of operational control by physically separating products that have not yet been released from inventory that are ready for distribution. Beyond supporting product segregation, this approach helps improve inventory management, simplify quality assurance processes and reduce unnecessary product handling.
Determining when a dedicated quarantine cold room becomes the more appropriate solution requires businesses to evaluate operational workflows rather than storage capacity alone. As pharmaceutical operations become larger and more complex, the ability to manage different inventory statuses efficiently becomes an increasingly important part of facility planning.
Quarantine Storage Supports More Than Product Segregation
Quarantine storage is commonly associated with preventing unreleased products from mixing with approved inventory. Although this remains one of its primary functions, a dedicated quarantine cold room also improves operational visibility throughout the pharmaceutical supply chain.
Products awaiting laboratory testing, quality review or regulatory approval often remain in storage for varying periods. Housing these products in a dedicated refrigerated environment allows warehouse personnel and quality assurance teams to manage inventory more efficiently without affecting released stock.
Consider a pharmaceutical distribution centre receiving imported vaccines from multiple manufacturers. Products arriving on different dates may require separate documentation reviews and quality release procedures before entering commercial distribution. A dedicated quarantine cold room helps maintain clear physical separation while allowing each product batch to progress through the approval process according to its own schedule.
This approach simplifies inventory control while reducing the likelihood of operational errors during busy warehouse activities.
Operational Growth Often Changes Storage Requirements
Dedicated quarantine cold rooms are rarely required because of a single increase in inventory. More commonly, they become necessary when operational complexity begins affecting warehouse efficiency.
As pharmaceutical businesses introduce additional product categories, expand distribution activities or increase storage capacity, warehouse teams manage larger numbers of product batches at different stages of approval. Existing refrigerated storage may continue providing sufficient capacity, yet the process of identifying, tracking and segregating inventory becomes increasingly difficult.
Project teams should therefore evaluate operational indicators rather than storage volume alone. Frequent movement of quarantine products, temporary storage arrangements or repeated changes to shelving layouts often indicate that the current facility no longer supports efficient inventory management. Planning a dedicated quarantine cold room before these challenges affect daily operations allows businesses to improve workflow while maintaining stronger control over temperature sensitive products.
Planning Quarantine Cold Rooms Around Operational Workflow
A quarantine cold room should support the movement of products through quality assurance processes rather than simply providing additional refrigerated space. Products entering quarantine should follow a logical workflow from receiving through inspection, documentation review, quality release and eventual transfer into approved inventory. Designing the cold room around this sequence helps reduce unnecessary handling while supporting more efficient warehouse operations.
Location also plays an important role. Positioning quarantine storage close to receiving areas and quality inspection activities can reduce transport distances while improving coordination between warehouse personnel and quality assurance teams.
Recognising When Existing Cold Rooms No Longer Support Quarantine Operations
Many pharmaceutical facilities begin by allocating dedicated shelving or clearly identified sections within an existing cold room for quarantine products. This arrangement can work effectively while inventory volumes remain manageable and product release activities are relatively straightforward. As operations expand, however, these temporary arrangements often become increasingly difficult to maintain.
One indication that a dedicated quarantine cold room should be considered is when products awaiting quality release begin competing for space with approved inventory. Warehouse personnel may need to relocate products repeatedly to accommodate new deliveries, while quality assurance teams spend additional time verifying inventory locations before inspections or product release.
Another sign is the increasing reliance on temporary storage practices. If quarantine products are regularly transferred between different storage locations because of limited space or changing operational priorities, the risk of handling errors and unnecessary product movement also increases. Reviewing these operational patterns allows businesses to determine whether existing refrigerated storage continues supporting quality assurance activities or whether a dedicated quarantine solution would provide greater long term efficiency.
Planning Considerations for Pharmaceutical Quarantine Cold Rooms
A dedicated quarantine cold room should support both product integrity and efficient operational workflows. The following considerations are commonly reviewed during the planning stage. Rather than viewing these requirements independently, pharmaceutical businesses should consider how each element contributes to a more efficient and controlled product release process.
|
Planning Consideration |
Why It Matters |
Operational Benefit |
|
Dedicated product segregation |
Prevents quarantine stock from mixing with released inventory |
Improves inventory control |
|
Controlled access |
Restricts handling to authorised personnel |
Strengthens operational discipline |
|
Logical location within the facility |
Supports efficient movement between receiving, quality assurance and storage |
Reduces unnecessary handling |
|
Environmental monitoring |
Maintains consistent storage conditions during quarantine |
Protects temperature sensitive products |
|
Flexible storage capacity |
Accommodates changing inventory volumes |
Supports future operational growth |
|
Clear inventory identification |
Simplifies batch tracking and quality release activities |
Improves traceability |
Supporting Future Facility Expansion
Quarantine storage requirements often increase alongside business growth. New product registrations, additional suppliers, expanded warehouse capacity and larger distribution networks all influence how pharmaceutical inventory is managed before release.
Planning a dedicated quarantine cold room as part of a broader facility strategy allows businesses to respond more effectively to future operational changes. Additional storage capacity, revised workflows and expanded quality assurance activities can be incorporated without significantly disrupting existing warehouse operations.
Future planning should also consider digital inventory systems and environmental monitoring infrastructure. Integrating these technologies during the initial design stage provides better operational visibility while supporting efficient inventory management as pharmaceutical facilities continue to expand. By considering future operational requirements instead of immediate storage needs alone, businesses can develop quarantine facilities that remain effective over the long term.
Developing a Quarantine Storage Solution That Matches Operational Requirements
Every pharmaceutical facility follows different quality assurance procedures, inventory profiles and product release workflows. For this reason, quarantine storage should be designed around operational requirements rather than adopting a standard cold room configuration.
Kiat Lay provides Custom Cold Room solutions that help pharmaceutical businesses develop refrigerated storage tailored to their quality assurance processes, warehouse layouts and future operational requirements. For larger pharmaceutical manufacturing or distribution facilities, Industrial Cold Rooms Storage Design For Multi Story Factories supports integrated cold storage planning that improves workflow, product segregation and long term operational efficiency.
Conclusion
A dedicated pharmaceutical quarantine cold room becomes increasingly valuable as pharmaceutical operations grow in scale and complexity. While standard refrigerated storage may be sufficient during the early stages of operation, expanding product portfolios, more demanding quality assurance procedures and increasing inventory volumes often require a more structured approach to quarantine management.
Planning quarantine storage around operational workflows rather than storage capacity alone helps improve product segregation, simplify inventory control and support more efficient quality assurance activities.
Contact Kiat Lay today to discuss your pharmaceutical cold storage requirements or request a consultation to develop a customised quarantine cold room solution that supports compliance, operational efficiency and future facility expansion.